
Industrial Epoxy Paint & Polyurethane Coating
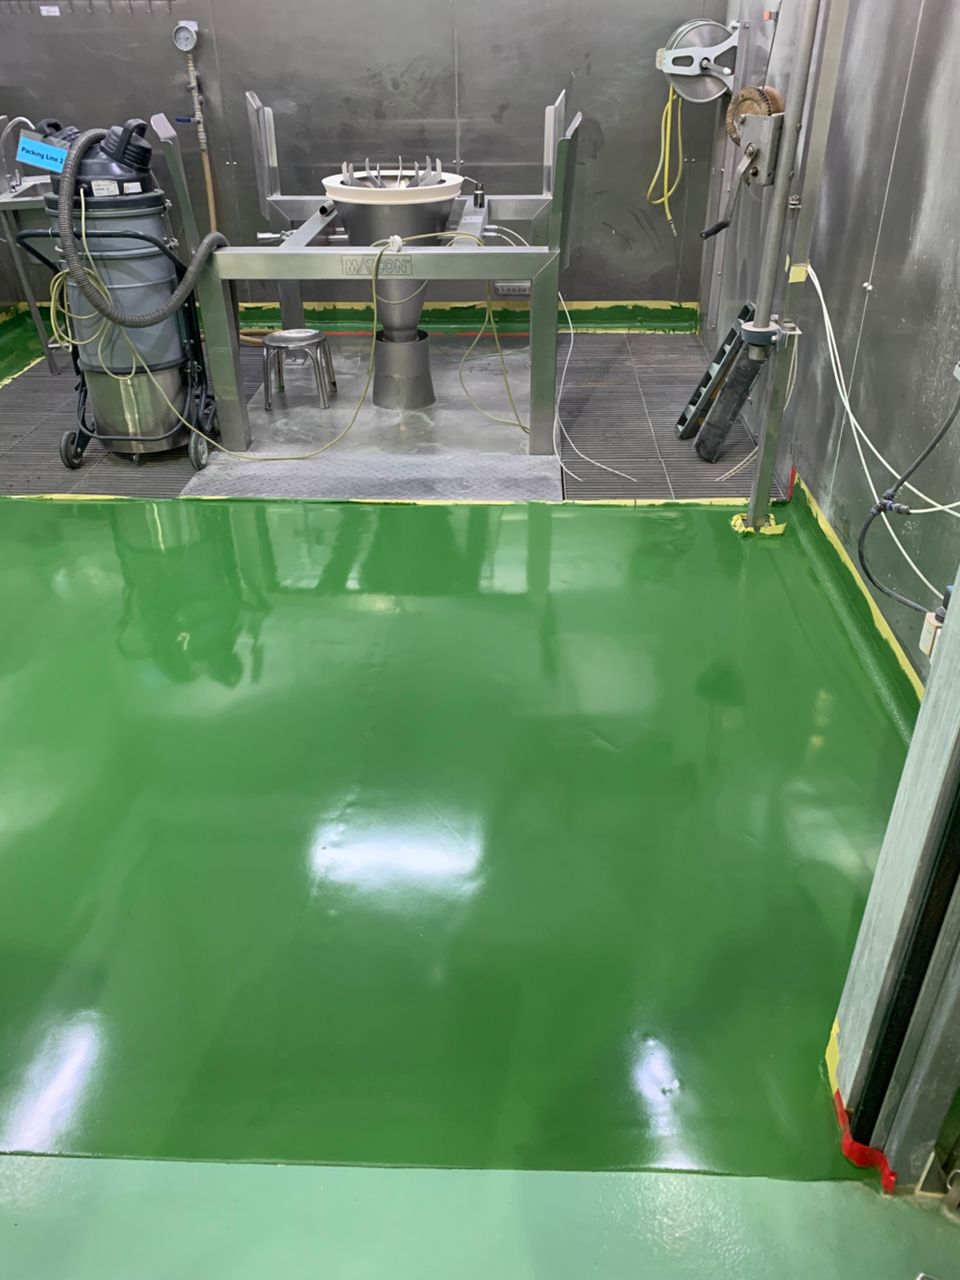
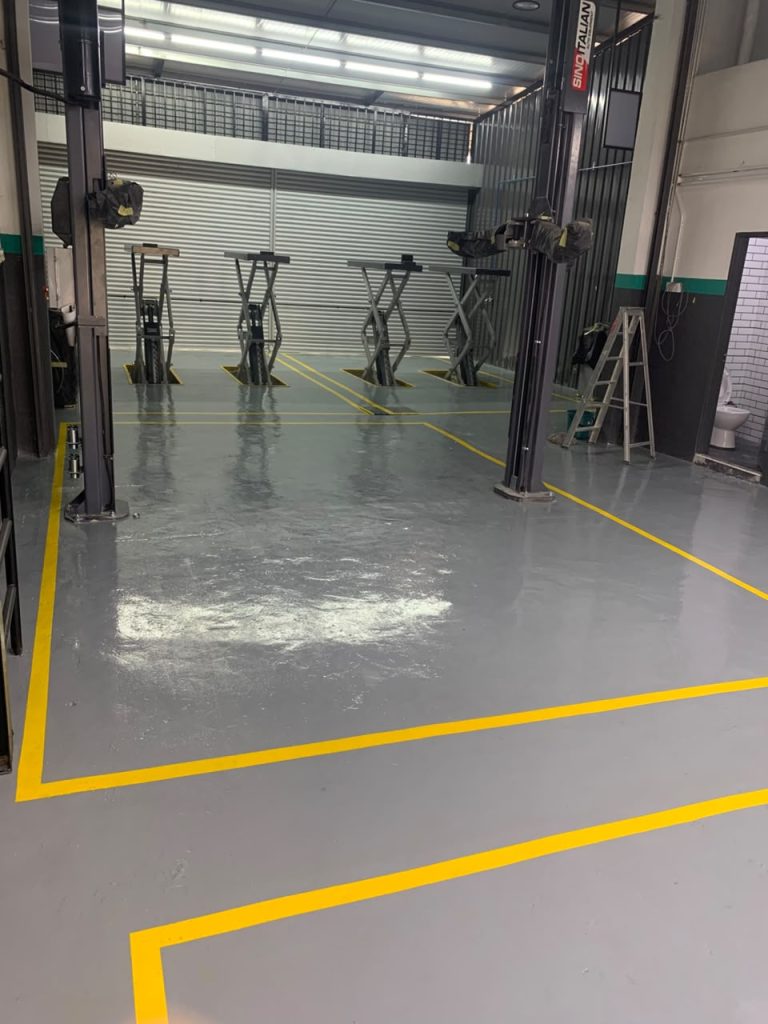
Industrial epoxy floor coating is a highly durable and versatile flooring system widely used in factories, warehouses, workshops, food processing plants, laboratories, pharmaceutical facilities, commercial buildings, and other heavy-duty industrial environments. It offers exceptional adhesion, chemical resistance, abrasion resistance, and mechanical strength, making it ideal for protecting concrete floors against traffic, impact, oil, chemicals, and daily wear.
Our industrial flooring solutions are available in a comprehensive range of epoxy and polyurethane coating systems to suit different operational requirements and floor conditions, including environments that require GMP (Good Manufacturing Practice) and HACCP (Hazard Analysis and Critical Control Point) compliance considerations for hygiene, cleanliness, and food safety.
Primer Systems
Solvent Free Epoxy Primer (SF Primer) – Low odor and suitable for high-performance industrial flooring systems.
Water Borne Epoxy Primer (P-250 WB) – Environmentally friendly primer with good bonding properties for damp or sensitive areas.
Epoxy & Polyurethane Finish Coatings
We provide various industrial-grade finish coatings depending on the required durability, appearance, and slip resistance:
- Self-Leveling Epoxy Floor Coating (SL-201) – Creates a smooth, seamless, and easy-to-clean surface for industrial and commercial floors.
Solvent Based High Gloss Epoxy Coating (FC-450) – Provides a glossy, attractive finish with strong surface protection.
Solvent Based Polyurethane Coating (FC-350) – Offers superior UV stability, flexibility, and long-term wear resistance.
Water Based Self Leveling Epoxy Floor Coating (SL-261WB) – Low-odor self-leveling system suitable for environmentally sensitive areas.
Polyurethane Mortar Screed Systems
For demanding industrial environments exposed to heat, moisture, chemicals, and heavy traffic:
- Self-Smoothing Polyurethane Screed (PU-MF) – Smooth polyurethane flooring system with excellent thermal shock and chemical resistance.
Suitable for GMP & HACCP Environments
Our seamless epoxy and polyurethane flooring systems are suitable for facilities that operate under GMP and HACCP requirements, including:
Food & beverage processing plants
Central kitchens and catering facilities
Pharmaceutical manufacturing areas
Cosmetic and healthcare production facilities
Clean rooms and hygiene-sensitive environments
The seamless, non-porous surface helps minimize dust accumulation, bacterial growth, and contamination risks while allowing easier cleaning and sanitization procedures required by GMP and HACCP quality management systems.
With the right combination of epoxy primers, self-leveling coatings, anti-slip finishes, epoxy mortar, and polyurethane screed systems, industrial floors can achieve long-lasting protection, improved safety, easier maintenance, enhanced hygiene performance, and a professional seamless appearance that performs reliably even under the toughest operating conditions.
Advantages of Industrial Epoxy Paint & Polyurethane Coating
Durability
Epoxy paint provides a hard, resilient finish that is resistant to abrasion, impact, and wear, making it ideal for high-traffic areas.
Chemical Resistance
It is highly resistant to chemicals, including acids, alkalis, solvents, and oils, making it suitable for environments where chemical spills are common.
Adhesion
Epoxy adheres well to a variety of substrates, including metal, concrete, and wood, ensuring long-lasting protection.
Moisture Resistance
It provides an impermeable barrier that protects surfaces from moisture, reducing the risk of corrosion and damage.
Temperature Tolerance
Epoxy coatings can withstand high temperatures, making them suitable for industrial environments with fluctuating temperatures.
Common Uses Area
Floor Coatings
Commonly used in industrial floors, warehouses, and factories where durability and chemical resistance are crucial.
Marine Environments
Used on ship decks, docks, and offshore platforms due to its excellent water and salt resistance.
Industrial Equipment
Protects machinery, pipelines, and storage tanks from corrosion and chemical exposure.
Automotive Industry
Applied to parts and components to enhance durability and resistance to chemicals and wear.
Let’s work together on your next flooring project
Contact us for your FREE QUOTATION and we will give FREE FLOOR TRAP
replacement to stainless steel for first 100 customers in 2024